


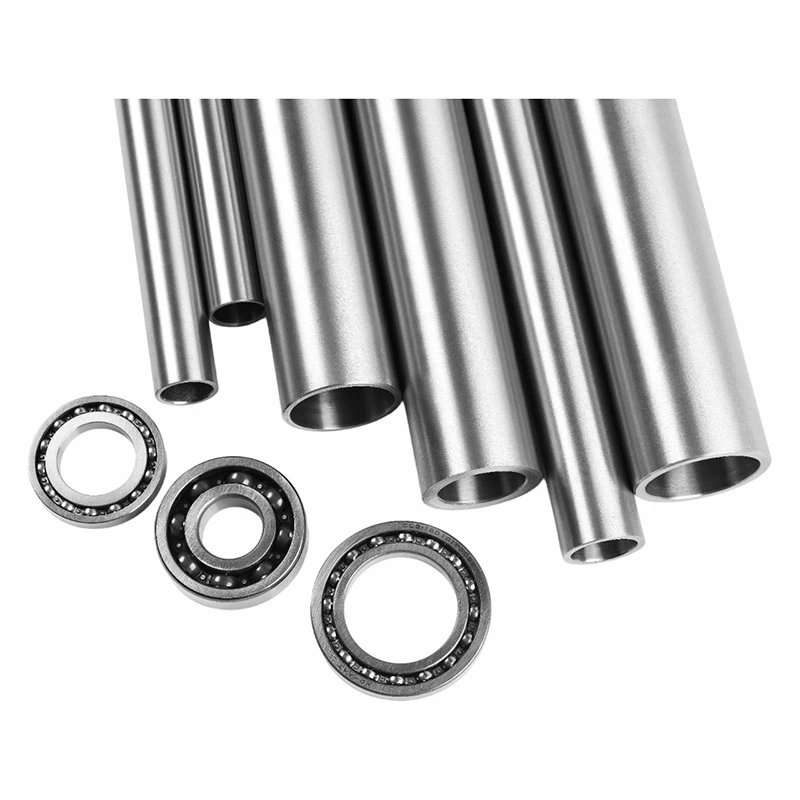
Precision thick-wall steel tubes are manufactured through cold drawing or cold rolling processes, yielding superior dimensional accuracy and mechanical properties compared to standard hot-rolled alternatives. Featuring heavy wall sections relative to their outer diameters, these tubes withstand high internal pressures and severe mechanical stress without deformation.
Manufacturing Advantage: Utilizing multi-pass cold drawing benches and controlled atmosphere annealing furnaces to eliminate internal stresses and ensure uniform microstructure.
Key Benefit for Procurement: Reduced machining time and material waste due to tight standard tolerances on both outer and inner diameters.
Specifications
|
Parameter |
Standard Range / Options |
|
Outer Diameter (OD) |
20 mm - 355 mm |
|
Wall Thickness (WT) |
3 mm - 50 mm |
|
Length |
5.8 m - 12 m (Fixed or random lengths available upon request) |
|
Dimensional Tolerances |
In accordance with EN 10305-1 / DIN 2391 (e.g., typical OD/ID precision tolerance classes like D4/H4 or customized tight tolerances upon agreement) |
|
Surface Finish (As-drawn / Annealed) |
Bright finish, free of heavy scale; Ra ≤ 1.6 μm (custom internal honing down to Ra 0.2 μm - 0.4 μm available) |
|
Manufacturing Standards |
ASTM A519, EN 10305-1, DIN 2391, JIS G3445 |
|
Steel Grades |
E355, ST52, 4140 (SCM440), 20#, 45#, 34CrMo4 |
|
Delivery Conditions |
+C (cold drawn/hard), +LC (cold drawn/soft), +SR (stress relieved), +A (annealed), +N (normalized) |
Material & Manufacturing
Material integrity directly dictates performance in high-pressure environments. Our production relies on fully traceable raw materials sourced from certified mills.
Steel Melting: Killed steel process utilizing Electric Arc Furnace (EAF) followed by Ladle Furnace (LF) refining and Vacuum Degassing (VD) to minimize sulfur, phosphorus, and non-metallic inclusions.
Cold Drawing Process: Drawn on hydraulic benches ranging from 100 to 500 tons, ensuring controlled cold work hardening and exact cross-sectional reduction.
Thermal Treatment: Roller hearth bright annealing furnaces with protective nitrogen/hydrogen atmospheres prevent oxidation and decarburization, ensuring consistent hardness across the entire wall thickness.
Quality Inspection
Every production lot undergoes rigorous mechanical and non-destructive testing prior to dispatch to meet international industrial benchmarks.
Dimensional Verification: Laser-based outer diameter and wall thickness gauges measuring continuous lengths.
Non-Destructive Testing (NDT): 100% Eddy Current testing and Ultrasonic testing (UT) performed in accordance with ASTM E213 / EN 10246-7 to detect longitudinal and transverse flaws.
Mechanical Testing: Tensile testing, yield strength verification, elongation measurement, and Brinell/Rockwell hardness testing per lot.
Metallographic Analysis: Grain size determination and inclusion rating conducted via optical microscopy.
Applications
Hydraulic Systems:
Cylinder barrels, piston rods, and high-pressure fluid transfer lines requiring zero leakage under cyclic loading.
Automotive Sector:
Drive shafts, axle housings, suspension components, and steering columns.
Mechanical Engineering:
Heavy-duty rollers, bearing sleeves, gear blanks, and structural columns in construction machinery.
Energy Sector:
Downhole drilling components and high-pressure valve bodies.
Customization & Supply
We support custom manufacturing requirements tailored to specific project blueprints and technical delivery conditions (TDC).
Custom Dimensions: Non-standard outer diameters and exact wall thickness ratios machined or drawn to print.
Surface Treatments: External/internal anti-rust oil coating, phosphating, shot blasting, or rough turning/peeling for subsequent machining.
End Finishes: Plain square cut, deburred, or bevelled ends prepared for welding.
Packaging: Bundled with steel strapping, wrapped in waterproof woven plastic, or packed in wooden crates for export transit protection.
FAQ
Q: What is the typical minimum order quantity (MOQ) for non-standard thick-wall dimensions?
A: MOQ depends on the steel grade and outer diameter. Typically, custom production runs start at 3 to 5 metric tons per size to account for setup and raw material rolling minimums.
Q: How do you control eccentricity in thick-wall tubes?
A: Eccentricity is minimized through precise mandrel positioning during the cold drawing process and verified using ultrasonic wall thickness scanning across 360 degrees of the circumference.
Q: Are mill test certificates provided with shipments?
A: Yes. EN 10204 3.1 Mill Test Certificates containing chemical composition, mechanical test results, NDT logs, and heat numbers are supplied with every order.
Q: Can these tubes be supplied in a fully machined or honed condition?
A: Yes. We offer internal honing (Ra 0.2 μm - 0.4 μm) for hydraulic cylinder applications, as well as external peeling or centerless grinding.
Q: What is the standard production lead time?
A: Standard stock items ship within 7–10 days. Custom cold-drawn production runs typically require 25–35 days depending on mill scheduling and heat treatment requirements.
Q: What third-party inspection agencies do you work with?
A: We routinely accommodate inspections by SGS, BV, TUV, Intertek, or client-specified designated third-party inspection bodies.
Request a Quote
Submit your technical specifications to receive a formal quotation within 24 hours. Please include the following details for an accurate response:
1.Steel Grade / Standard (e.g., EN 10305-1 E355)
2.Dimensions: Outer Diameter (OD) × Wall Thickness (WT) × Length
3.Quantity (Metric Tons or Pieces)
4.Delivery Condition (+C, +SR, +N, etc.)
5.Target Port of Destination / Incoterms (FOB / CIF / DDP)
[Submit Technical Inquiry / Request RFQ]
Hot Tags: precision thick-wall steel tubes, China precision thick-wall steel tubes suppliers, factory


